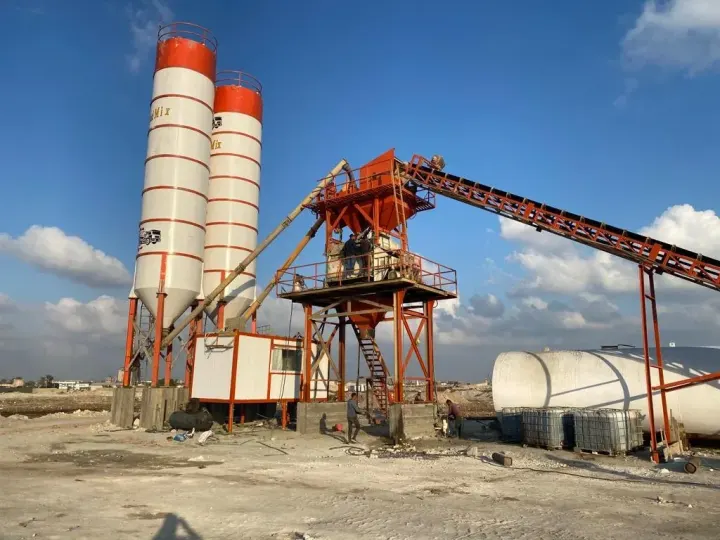
A structured method to size a concrete batching plant using peak-day volume, pouring hours, truck fleet and growth plans, with an indicative guide to capacities from 60 to 130 m³/h.
Concrete plant capacity selection determines both your investment size and your ability to meet delivery commitments. In short, choose capacity based on peak-day pouring volume, actual pouring hours and truck fleet capability, plus a margin for growth, not on monthly averages. Mousa Sons offers plants rated at 60, 80, 100, 120 and 130 m³/h, and this article sets out a structured way to choose between them.
Rated vs Actual Capacity
Plant capacity is expressed in cubic metres per hour, but two figures matter:
- Rated capacity: the theoretical maximum under ideal conditions, as stated in the specification.
- Actual output: what the plant really produces on site, usually lower because of mixing time, recipe changes, truck waiting and cleaning.
The most common mistake is sizing a plant as if rated capacity will be achieved all shift long.
Key Inputs for Concrete Plant Capacity Selection
Peak-day volume
Demand is uneven. Slab and foundation pours require large volumes in limited windows. The plant must serve the peak day, because falling short means unplanned cold joints and quality issues.
Actual pouring hours
Heat, traffic restrictions or project rules may limit pouring hours. Fewer hours mean higher hourly capacity for the same daily volume.
Truck fleet and distance
A plant cannot effectively outproduce its truck mixers. Longer haul distances extend each truck's cycle and require more trucks to keep the plant running at capacity.
Mix designs
Some mixes need longer mixing or multiple admixtures, reducing cycles per hour.
Growth
Sizing only for today may force an early upgrade, while oversizing locks up capital. Balance is the goal.
A Step-by-Step Method
- Estimate peak-day pouring volume from current and planned projects.
- Divide by actual available pouring hours to get the required hourly output.
- Add a margin for the gap between rated and actual capacity.
- Add a growth margin based on your business plan.
- Select the nearest available capacity above the result.
- Check the balance between capacity, truck fleet and storage.
Indicative Guide to Available Capacities
| Capacity (m³/h) | Typical fit |
|---|---|
| 60 | Contractors starting in-house production, mid-sized projects |
| 80 | Contractors with steady workloads, emerging ready-mix plants |
| 100 | Commercial ready-mix with stable demand, large projects |
| 120 | Plants serving several projects with frequent peak days |
| 130 | National-scale projects and large continuous pours |
This table is indicative; the final decision depends on your project data. Explore configurations on our ready-mix concrete batching plants service.
Capacity Is More Than the Mixer
Upsizing the mixer without the rest of the system just moves the bottleneck. A balanced plant needs:
- Enough cement storage: our cement silos range from 60 to 180 tonnes.
- Aggregate bins and conveyors that feed the mixer without delay.
- Adequate water supply, with tanks of 50 and 75 m³ available.
- A fast, accurate control system to shorten cycle time.
Review the whole chain, from aggregate stockpiles to truck loading points, whenever you make a capacity decision. The weakest link determines what the plant really delivers.
Market Conditions in Egypt and the Region
Peak demand often follows major project cycles and construction phases in new cities. High summer temperatures also restrict pouring to cooler hours on many sites, compressing the same volume into a shorter window and raising the required hourly output. Haul distances, road conditions and traffic affect truck cycle times too, and should be modelled carefully when choosing between two close capacity options.
One Large Plant or Two Smaller Ones?
Splitting capacity across two smaller plants at different locations can outperform one large plant when projects are geographically spread or when continuity is critical. Two plants provide redundancy during maintenance and shorten haul distances. A single large plant, on the other hand, is simpler to manage, easier to quality-control and needs fewer staff. The right answer depends on where your projects are and how sensitive your operation is to downtime.
Still deciding on the plant type itself? Read our stationary vs mobile comparison and the complete buying guide.
Frequently Asked Questions
Can capacity be increased later?
Often yes, through mixer, weighing or control upgrades or additional silos via our plant upgrade and modernization service, although planning ahead is always more economical. See when upgrading beats buying new.
Is higher capacity always better?
No. Unused capacity means idle capital and higher running costs without a return.
How does the mixer affect capacity?
Mixer size and efficiency set batch volume and mixing time, and therefore cycles per hour.
Does operator training affect actual output?
Yes. Well-trained operators shorten cycle times, reduce weighing errors and minimise stoppages, bringing actual output closer to rated capacity.
Size Your Plant With Our Team
Send us your peak-day volume, working hours and fleet size, and our engineers will help you select the right capacity. Request an estimated quotation today.